2026-10-31
Race and Rally Car Preparation in Northampton: The Engineering Behind a Car That Finishes
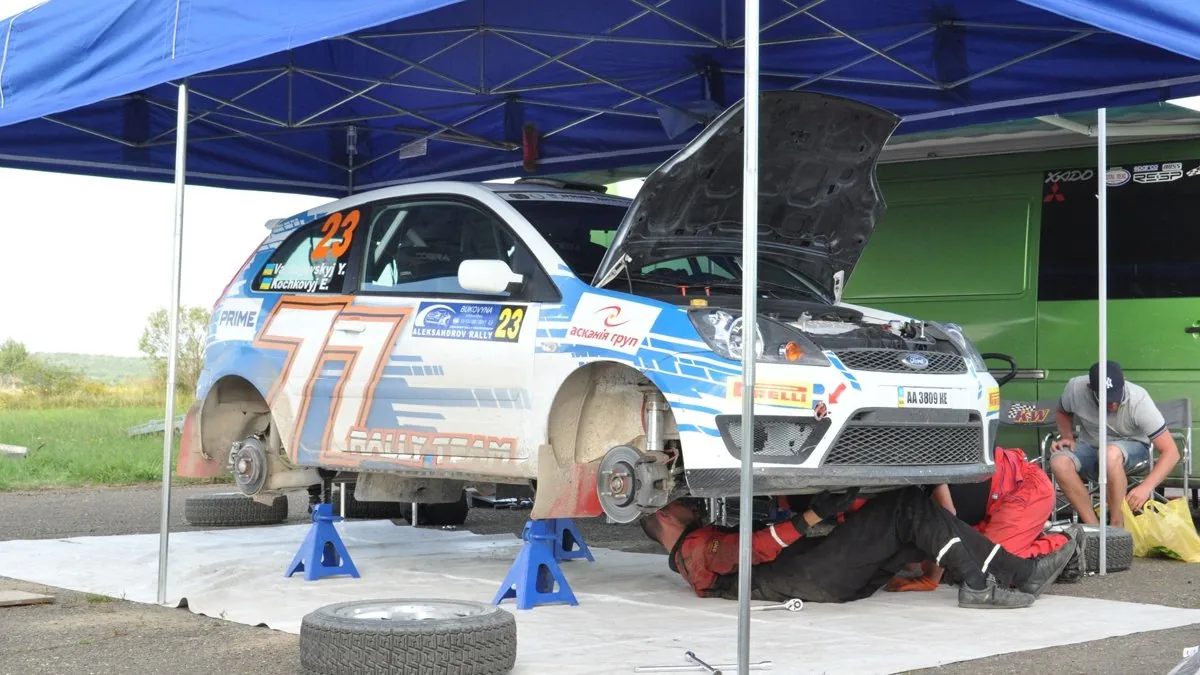
A properly prepared race or rally car is one where every number is known, recorded and repeatable: the cross-weights, the corner heights, the camber and toe, the fuel cell's date of manufacture, the torque on every cage joint, and the air-fuel ratio at every point on the map. "Close enough" doesn't survive a scrutineering bay or a 90-minute race. Get the preparation wrong and you either fail paperwork, lose the car to a reliability DNF, or leave lap time on the table because the chassis was never set up to use the tyre.
Northampton sits at the heart of the UK motorsport cluster — minutes from Silverstone, surrounded by fabrication shops, engine builders and race teams — so the standard here is high. This is a practitioner's guide to what race and rally car preparation in Northampton actually involves: the safety structure, the fuel system, the chassis setup, and the engine and calibration work that turns a built car into a repeatable one. I'll be straight about which jobs are regulation-driven, which are performance-driven, and where the two overlap.
Start with the rulebook: safety cage specification
The safety cage (ROPS) is the one area where creativity gets you excluded. The governing documents are FIA Appendix J, Articles 253 and 254, plus Motorsport UK's Section K regulations. A safety cage is a structural framework designed to prevent serious bodyshell deformation in a collision or rollover — it is not a styling bar.
There are three legal routes to a compliant cage: it's legal by being built to the published specification, by carrying an ASN certificate, or by being FIA homologated. If you go the build-to-spec route, the material and minimum tube sizes are fixed:
| Member | Minimum tube size | Material |
|---|---|---|
| Main hoop | 45 × 2.5 mm or 50 × 2.0 mm | Cold-drawn seam-free unalloyed carbon steel, max 0.3% carbon |
| Other members | 38 × 2.5 mm or 40 × 2.0 mm | As above; circular section only |
Aluminium alloy roll cages are prohibited outright. If removable members are used, the demountable joints must comply with an approved type (drawings K21–K30), and bolts must be ISO 8.8 or better. Crucially, demountable joints must not be used as part of a main, front or lateral rollbar — they act as hinges and allow the structure to deform under load.
CDS versus T45 — the point everyone gets wrong
CDS means cold-drawn tube with no seam — it describes how the tube is made, not what it's made from. T45 (BS4 T45) is a carbon-manganese steel that is also cold-drawn and seam-free. Neither the FIA nor Motorsport UK names T45 in the regulations. The strength difference is real — a published minimum of 620 N/mm² yield for T45 against 370 N/mm² for a high-spec CDS — but here's the catch: on a cage built to the published specification, the minimum tube sizes apply whatever the steel is. T45 buys you no dimensional allowance.
Thinner-wall T45 is only legal where that specific cage design is FIA homologated or holds a Motorsport UK ROPS Certificate. The weight prize is worth having — CDS at 45 × 2.5 mm is roughly 2.69 kg/m, so around 20 m of tube is near 54 kg, while T45 at 45 × 1.6 mm is about 1.7 kg/m, or roughly 34 kg, a saving in the region of 20 kg. But those are vendor marketing figures and depend entirely on cage design. You only unlock them with the right paperwork, not by swapping steel and hoping.
And do not modify a certified or homologated cage. The FIA is blunt: any modification is forbidden, and machining or welding that permanently changes the material or the cage counts. Keep an authentic copy of the homologation document or certificate available for scrutineers, and leave the identification plate exactly where it was fixed.
Fuel cells: the component with an expiry date
A safety fuel cell is the part most privateers forget to track. FT3-1999 is the minimum standard for WRC, Regional Rally, Circuit and most Drift championships. The FT3 standard mandates a flexible bladder contained within a rigid box — typically ballistic nylon fabric, impregnated and twice-coated with fire-retardant polyurethane elastomers, and baffled with polyurethane safety foam to suppress an explosion in the vapour space.
The date that matters is manufacture, not purchase. All sanctioning bodies limit use to 5 years from the date of manufacture, per FIA FT3-1999 section 2: no bladder is used for more than 5 years unless reinspected and recertified by the manufacturer. After 5 years the tank can be returned for inspection; if the bladder is healthy it is re-homologated for a further 2 years. Typical physical lifespan is 8–10 years, but the regulation caps you well short of that.
If you run E85, read this twice
Foam life depends heavily on fuel. Vendor guidance puts yellow foam with pump gas or avgas at 5–10 years, but yellow foam with E85 at only 3–6 months — that's a genuine safety danger, because degraded foam breaks up and blocks pickups and vents. Black spec-E85 foam with E85 is rated for 5 years plus. These are manufacturer figures, so confirm against your specific cell and championship regs, but the principle holds: match the foam to the fuel. And empty the tank after every event — it makes a measurable difference to the life of both the foam and the bladder.
Corner weighting and chassis setup: where lap time lives
Within many categories, corner weighting before an event has a large effect on lap times and the car's balance. Done properly, it's one of the highest-value preparation jobs there is — and one of the easiest to botch.
The non-negotiable is race trim. The car must be in the same state it would race in: driver in the seat, correct fuel load, splitters attached, cool-suits filled. No driver? Fill the seat with ballast at the exact dressed weight of the driver, helmet included. Fuel strategy matters too — a common approach is to fill to half the level you start the race with, so the car is balanced at the optimum performance mass in the middle of the race. You can bias the setup to the start, middle or end depending on strategy, but decide deliberately.
The procedure essentials:
- Scales on a perfectly flat, even surface; finely adjustable ride height at each corner (adjustable coilovers).
- Set race tyre pressures.
- Disconnect the anti-roll bar so it can't pull the opposite side and skew corner mass.
- Bounce each corner to free the suspension from bind, then roll — never jack — the car onto the scales.
- Make small changes at each corner, not one big change at a single corner.
Understand the physics before you touch a spring platform. Lowering ride height at a corner loses weight at that corner and the diagonally opposite one; raising it adds weight. Cross (diagonal) weight is the most important component, and for most circuit work the goal is equal cross-weights — LF + RR = RF + LR. Oval and circle-track setups deliberately run unequal cross-weight, or "wedge". Remember too that static weight can only be changed by physically moving mass around the car — spring adjustments redistribute, they don't relocate. When you've finished, reconnect the anti-roll bars and shim the drop links so there's no static twist on the bars, with the driver in the car.
Geometry to suit the tyre
Wheel alignment on a competition car isn't a four-wheel laser check against factory numbers. The aim is to optimise geometry for your suspension and tyre type to extract maximum performance, and the right figures are track- and condition-specific. Tarmac rally, gravel and circuit all want different camber and toe, and the only honest way to dial it in is to set, run, read the tyre temperatures and adjust.
Engine and calibration: making the power repeatable
A car that's safe and well set up still needs an engine that makes its power the same way every lap and finishes the race. That's a build discipline before it's a tuning one — see our guide on what actually separates a built engine from a bodged one and on how to build a legal, repeatable engine that finishes races.
On the induction side, this is where component choice directly feeds preparation quality. A properly sized and positioned individual throttle body (ITB) and intake setup is the difference between a peaky dyno hero and a drivable, repeatable race engine — the detail is in our pieces on sizing and plumbing injectors and ITBs and on choosing a Peugeot XU throttle body kit that fits your head. As a real-world data point, a Peugeot 306 GTI-6 fitted with our throttle bodies and mapped made 183.4 bhp — a single build, not a blanket spec, but representative of what a properly matched induction system and calibration return.
Intake geometry: printed carbon composite as a serious option
Intake parts are where preparation meets manufacturing route. The traditional path is a laminated — prepreg/autoclave — composite or a machined aluminium part. We also print our intake components in carbon composite (PPA-CF, carbon-fibre-reinforced polyphthalamide) using direct digital manufacturing (DDM), and for a lot of race applications the printed part wins on engineering grounds, not marketing ones:
- Geometry you cannot otherwise make. Printing lets us create hollow, closed internal cavities, tuned-length runners and smooth internal transitions in one piece — shapes you simply can't laminate or machine. Pressure-wave tuning lives in that runner geometry, so being free to optimise it is a direct performance lever.
- Thermal insulation where it counts. A reinforced polymer plus a trapped-air cavity picks up far less heat into the intake charge than aluminium (density 2.70 g/cm³, thermal conductivity 150–220 W/m·K — orders of magnitude higher than the polymer). That benefit is biggest at idle and heat-soak in the paddock and on the grid; at sustained wide-open throttle the advantage narrows. I'll tell you honestly which case applies to your car.
- Weight. PPA-CF is 1.25 g/cm³ — under half aluminium's 2.70 g/cm³ before the hollow section is even counted.
- Genuine port matching. The part is designed around your head and your combination — no universal-fit compromise.
- CAD-to-dyno speed. We iterate geometry in days, so shapes are optimised on real data, not on a catalogue.
On heat: don't fixate on the 85°C glass transition. PPA-CF is semi-crystalline and fibre-reinforced, so it keeps load-bearing capability well above Tg — which is why its heat deflection temperature is 196°C at 1.8 MPa and 227°C at 0.45 MPa (ISO 75), with a Vicat softening point of 232°C. For under-bonnet service, the HDT is the number to lead with. Mechanically it runs 168±4 MPa tensile and 11,800±670 MPa Young's modulus in XY, with bending strength 208±6 MPa and impact strength 41.7±2.8 kJ/m².
Where is a laminated/autoclave part genuinely the right call? Very high sustained temperatures, or any part where Z-axis strength governs — printed PPA-CF is 57±5 MPa tensile in Z against 168 MPa in XY, so orientation matters and it has to be designed in. That's the honest contrast: laminated composite versus printed carbon composite, each reached for when the engine calls for it. More detail in our articles on the carbon intake manifold that actually works and specifying custom components that fit and last.
Mapping that holds up
Calibration ties it together. A map developed on a rolling road in isolation isn't the same as one developed with knowledge of the fuel, the cooling, the duty cycle and the mechanical limits of the build. Our approach to that — and what proper mapping actually involves — is covered in how proper race engine calibration works. If you're booking track time to validate a setup, the UK and European trackday list is a useful place to plan around.
FAQ
Is a T45 roll cage automatically legal because the steel is stronger?
No. On a cage built to the published specification, the FIA/Motorsport UK minimum tube sizes apply regardless of steel grade, so T45 gives no dimensional allowance. Thinner-wall T45 is only legal where that exact cage is FIA homologated or holds a Motorsport UK ROPS Certificate. Carry the paperwork.
How long can I run my fuel cell?
FT3-1999 bladders are limited to 5 years from the date of manufacture, not purchase. After that, the manufacturer can reinspect and re-homologate a healthy bladder for a further 2 years. Physical lifespan is often 8–10 years, but the regulation is the hard limit — and if you run E85, foam condition can force replacement far sooner.
Do I need a driver present for corner weighting?
You need the driver's weight in the seat. If the driver can't be there, ballast the seat to their fully dressed weight (helmet included), set race fuel and tyre pressures, disconnect the anti-roll bar, and roll the car onto level scales. The car must be in true race trim or the numbers are meaningless.
Is a printed carbon composite intake as strong as a laminated one?
For most race intake duty, yes — PPA-CF runs 168 MPa tensile and 196–227°C HDT, and the printed route unlocks hollow, tuned geometry you can't laminate. The exception is parts where Z-axis load or very high sustained temperature governs; there a laminated/autoclave part can be the better tool, and we'll say so.
Getting it done in Northampton
Preparation is the sum of a lot of small, measured jobs done to a standard rather than a feel. GMR is a Northampton-based motorsport engineering company, and our focus is the engineering end of that work — custom race engine and component manufacture, bespoke engine calibration for OEM and aftermarket ECUs, and intake and throttle body systems built around your specific combination rather than a universal-fit catalogue. Bring us the combination, the regulations you run under, and the result you need, and we'll engineer to it.